Download the 2025 Focal Car Catalogue | Focal INSIDE Catalogue | Join our Mailing List!

China Top Chocolate Processing Plant Manufacturers?

Choosing among China’s top Chocolate Processing Plant manufacturers requires more than comparing catalog prices. The right partner should demonstrate engineering experience, stable production records, and transparent quality controls. A modern Chocolate Processing Plant may include roasting, refining, conching, tempering, molding, cooling, and packaging equipment. Each stage affects viscosity, gloss, snap, aroma, and shelf life. Small details matter. Ask how manufacturers manage temperature accuracy, hygienic design, spare parts, and operator training. Factory visits or live video inspections can reveal cable routing, stainless-steel welds, floor drainage, and actual machine operation.

This article introduces leading Chinese manufacturers through practical selection criteria rather than an unverified ranking. Their capabilities may differ widely. Some focus on compact lines for startups, while others build high-output systems for industrial confectionery producers. Experienced suppliers should provide process flow diagrams, capacity calculations, energy estimates, installation plans, and validation documents. They should also explain whether the line handles dark, milk, white, or filled chocolate. Cocoa origin is important, but equipment performance cannot rescue poor tempering control. That point is often overlooked.

Reliable sourcing requires evidence. Review certifications, export experience, customer references, warranty terms, and after-sales response times. Request test samples using your recipe, including inclusions such as nuts or crisped rice. Measure throughput, product temperature, cleaning time, and waste. Results may be less impressive than brochures suggest. That is useful information. Buyers should compare total ownership cost, not only the initial quotation. Currency changes, shipping, commissioning, and replacement parts can alter the final budget. A careful evaluation helps manufacturers and buyers build safer, more consistent, and commercially practical chocolate production lines.
China Top Chocolate Processing Plant Manufacturers?

Chocolate Processing Plant Manufacturing in China

China Top Chocolate Processing Plant Manufacturers?

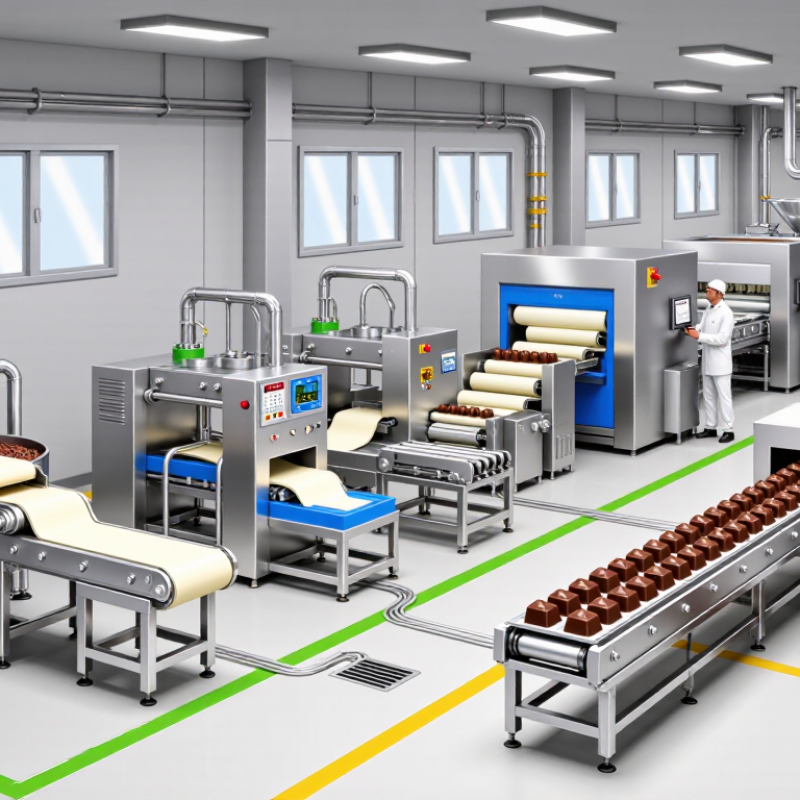
China’s chocolate processing plant manufacturing sector serves confectionery, bakery, and compound-coating production. A capable factory integrates roasting, grinding, refining, conching, tempering, molding, cooling, and packing. Each stage affects viscosity, snap, gloss, and shelf stability. Small deviations matter.

The International Cocoa Organization estimated 2023/24 cocoa production at 4.382 million tonnes, against grindings of 4.855 million tonnes. This projected shortfall makes yield control more important for Chinese processors. Modern lines use closed transfer pipes, heat recovery, automated temperature control, and clean-in-place systems. A tempering unit should hold narrow temperature bands, not merely display a target number. Operators still inspect test pieces under controlled light. Machines can be precise. People can misread them.

The USDA Foreign Agricultural Service’s China Retail Foods Annual report highlights e-commerce and premium retail as important food channels. Manufacturers should therefore document food-contact materials, calibration records, allergen separation, and batch traceability. HACCP-based controls and ISO 22000 systems strengthen supplier audits, although certification alone does not guarantee consistent chocolate. China’s GB 2760 standard also guides permitted additives and usage limits. Purchasers should request factory acceptance tests, sample runs, utility data, and maintenance training. Cooling-water quality is often overlooked; scale can quietly reduce performance. Some projects over-automate before stabilizing recipes and operator skills. That is an expensive lesson.

This chart shows representative temperature benchmarks commonly used across major chocolate-processing stages. Actual settings vary by cocoa origin, recipe, equipment design, and product specification; the data is presented as an industry-process reference rather than company or brand performance.

Key Equipment and Production Capabilities

A capable chocolate processing plant manufacturer should offer more than attractive machinery. The equipment must support stable quality from raw cocoa handling to finished products. Typical lines include roasting units, winnowers, grinders, mixers, refiners, and conches. Each machine affects flavor, texture, and production consistency.

The details matter.

A five-roll refiner can reduce particle size for a smoother mouthfeel. Conching equipment develops aroma while controlling moisture and viscosity. Tempering systems must maintain accurate temperature curves, often within a narrow operating range. Moulding machines should deliver consistent weights and clean release. For coated products, enrobing lines need steady chocolate flow and controlled cooling tunnels. Stainless steel contact surfaces, accessible inspection points, and reliable cleaning procedures are essential.

Good manufacturers also provide production testing. They should review cocoa recipes, hourly output, energy use, and available factory space before proposing a line. Sensors can monitor temperature, flow, and motor performance. Traceability systems help operators connect each batch with ingredients and process records. Practical training matters as much as installation.

No line is perfect. A design that performs well with dark chocolate may struggle with filled products. Small changes in fat content can affect tempering stability. I would request pilot trials before approving large equipment. Maintenance access is another commonly overlooked issue. Fast production means little when cleaning takes too long or replacement parts remain unavailable.

Leading Chinese Chocolate Processing Plant Manufacturers

China’s leading chocolate processing plant manufacturers serve factories of different sizes, from small bean-to-bar workshops to automated industrial lines. Experienced manufacturers usually provide roasting, winnowing, grinding, refining, conching, tempering, molding, and cooling equipment. Each stage affects flavor, texture, and production stability.

Strong manufacturers explain technical limits clearly. They discuss cocoa capacity, heating accuracy, energy use, cleaning procedures, and spare-part availability before quoting equipment. A reliable supplier may also arrange factory testing, installation guidance, operator training, and remote troubleshooting. These details matter when a tempering unit must hold a narrow temperature range during a busy production shift.

Practical experience is easy to notice. Engineers should understand sticky chocolate residue, uneven cooling, vibration, and seasonal changes in raw materials. Stainless steel contact surfaces should be easy to inspect and sanitize. Safety guards, emergency stops, electrical documentation, and local compliance support deserve careful review.

Not every “complete line” is equally complete. Some proposals look impressive but leave packaging, ventilation, or utility requirements unclear. Buyers should request process diagrams, output tests, maintenance schedules, and references from similar projects. A factory visit can reveal more than polished photographs. Check the workshop floor, test records, and response time.

There is room for doubt.

The best choice may not be the cheapest or the largest. It should match the product, workforce, budget, and future expansion plan. Even experienced buyers can overlook cleaning time, training needs, or installation delays. Careful comparison makes these weaknesses visible before production begins.

Quality Standards and Food Safety Certifications

A reliable chocolate processing plant proves quality through documented controls, not attractive machinery alone. During factory evaluations, I look for clear process maps, trained operators, and traceable ingredient records. Cocoa beans, sugar, milk powder, and emulsifiers should have approved supplier documentation. Every batch needs a lot number.

Food safety certification provides an important framework. HACCP identifies hazards at receiving, roasting, refining, conching, and packaging stages. ISO 22000 connects these controls with a wider food safety management system. Some plants also hold FSSC 22000 or BRCGS certification, depending on customer and market requirements. Certificates should be current, independently audited, and matched to the actual production site.

The details matter. Metal detectors need routine challenge tests. Temperature logs should show real readings, not copied numbers. Allergen controls must separate milk, nuts, and other sensitive materials. Cleaning records should include equipment contact surfaces and verification results. During an audit, I also check corrective actions after failures. Weak follow-up can reveal more than a polished certificate.

No system is perfect. A plant may pass an audit yet still struggle with staff turnover or rushed maintenance. That possibility deserves attention. Buyers should request recent audit findings, laboratory reports, recall procedures, and sample traceability exercises. A trustworthy manufacturer answers specific questions with evidence. Safety is built daily.

How to Select a Reliable Chinese Manufacturer

China Top Chocolate Processing Plant Manufacturers?

How to Select a Reliable Chinese Manufacturer

Selecting a reliable Chinese chocolate processing plant requires more than comparing prices. Visit the facility when possible, or request a live video inspection. Look for clean production areas, controlled temperatures, organized ingredient storage, and clear worker hygiene procedures. Ask how cocoa, milk powder, and other ingredients are received and traced.

Technical experience matters. A capable manufacturer should explain refining, conching, tempering, molding, and packaging without vague promises. Request production records, equipment maintenance plans, quality-control procedures, and recent test reports. Confirm whether the factory can manage your required output, recipe, packaging format, and minimum order quantity. Small trial batches are useful. They reveal texture, gloss, flavor stability, and delivery discipline.

Check communication carefully. Reliable teams answer specific questions, share realistic schedules, and identify possible production risks early. A factory that promises everything may understand little. I have found that sample approval alone is not enough; the approved sample can differ from mass production. Include measurable standards in the contract, such as weight tolerance, appearance, shelf-life testing, packaging materials, and inspection steps. Independent inspection can add confidence before shipment. Still, no audit removes every risk. Delays, raw-material changes, or unclear translations may create problems. Keep written records, approve each change, and review performance after every order.

China Top Chocolate Processing Plant Manufacturers? - How to Select a Reliable Chinese Manufacturer

Evaluation Dimension What to Verify Reliable Benchmark Recommended Evidence Warning Signs
Legal Manufacturing Status Confirm that the facility is legally registered and authorized to manufacture and export food products. The registered business scope should include food manufacturing, processing, or related activities. Business registration information, food production documentation, export records, and a current factory address. Only a trading address, inconsistent legal information, or refusal to provide documentation.
Food Safety Management Review the systems used to identify, control, and document food-safety hazards. A documented HACCP-based system, traceability procedure, sanitation program, and corrective-action process. Valid third-party audit reports, HACCP records, sanitation logs, pest-control records, and traceability tests. Generic certificates without scope, expired documents, or no batch-traceability procedure.
Certification Scope Check whether certifications cover the actual plant, product category, and manufacturing process. Certification scope should match chocolate, cocoa-based products, confectionery, or the specific product being ordered. Certificate number, issuing body, validity period, site address, product scope, and audit status. A certificate belonging to another site, unrelated product scope, or missing validity information.
Processing Capability Assess whether the plant can perform the required chocolate processes consistently. Suitable equipment for mixing, refining, conching, tempering, molding, enrobing, cooling, and packaging as required. Equipment list, process-flow diagram, factory video or audit, trial-production records, and product samples. Unclear process ownership, rented equipment without capacity details, or inability to conduct a production trial.
Product Quality Control Evaluate controls for ingredients, in-process parameters, finished products, and packaging. Written specifications for cocoa content, fat composition, viscosity, moisture, particle size, appearance, weight, and shelf life. Certificates of analysis, inspection plans, calibration records, retained samples, and nonconformance reports. Quality checks based only on visual inspection or no defined acceptance criteria.
Ingredient Traceability Determine whether raw materials can be traced from supplier and lot to finished-product shipment. Each production batch should link ingredients, packaging materials, processing records, and dispatch information. Lot-number examples, supplier approval records, receiving logs, and a completed mock recall. Unlabeled ingredients, incomplete batch records, or inability to identify affected shipments.
Allergen and Cross-Contact Control Review how the plant manages milk, soy, nuts, peanuts, gluten, and other declared allergens. Ingredient segregation, validated cleaning procedures, allergen labeling controls, and documented changeover checks. Allergen matrix, cleaning validation, environmental swab records, label approvals, and production scheduling rules. No allergen map, shared lines without risk assessment, or inconsistent label information.
Capacity and Delivery Reliability Compare available capacity with forecasted demand and seasonal production requirements. Capacity should be supported by equipment ratings, shift plans, lead-time estimates, and documented order history. Monthly capacity statement, production schedule, on-time delivery data, and contingency plan for peak seasons. Unusually large capacity claims without equipment evidence or frequent unexplained delivery delays.
Customization and Minimum Order Quantity Clarify support for recipe development, mold design, packaging, private-label production, and pilot orders. The supplier should state minimum order quantities, tooling charges, sample fees, revision limits, and approval stages in writing. Quotation, product-development timeline, approved sample, packaging specification, and signed technical agreement. Hidden tooling costs, unclear sample ownership, or major changes in price after approval.
Export and Regulatory Compliance Verify that the supplier can meet the destination market’s ingredient, labeling, packaging, and documentation requirements. Product specifications and labels should be reviewed against the importing country’s applicable food regulations before mass production. Ingredient statement, nutrition data, allergen declaration, shelf-life validation, laboratory reports, and shipping documents. Supplier claims that one label works for every market or cannot provide product-specific documents.
Facility Hygiene and Working Conditions Inspect zoning, personnel hygiene, material flow, cleaning, pest control, and temperature management. Cleanable surfaces, controlled access, separated raw and finished-product areas, documented cleaning, and suitable storage conditions. On-site audit, dated facility photographs, hygiene records, pest-control reports, and warehouse inspection. Visible contamination risks, poor housekeeping, uncontrolled storage, or refusal of an independent audit.
Commercial Transparency and After-Sales Support Assess communication, contract clarity, complaint handling, replacement policy, and technical support. Clear quotations, agreed specifications, payment terms, delivery responsibilities, complaint-response times, and corrective-action procedures. Signed sales contract, quality agreement, service contacts, complaint records, and independently verified customer references. Pressure for full payment, vague contracts, inconsistent communication, or refusal to accept quality claims.

Note: Certification requirements, labeling rules, import documents, and testing obligations should always be confirmed for the destination market and specific chocolate product.